Send Inquiry
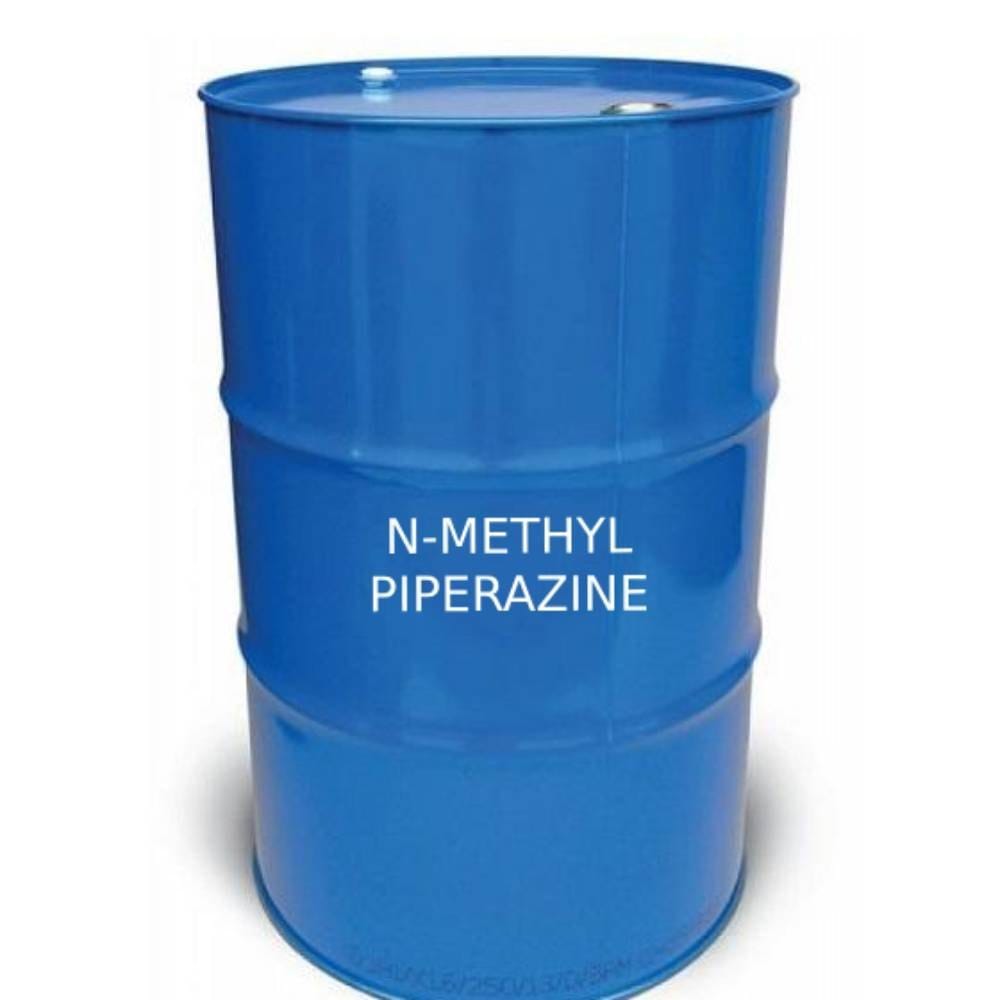
N- methylpiperazine

N- methylpiperazine Specification
- Solubility
- Miscible with water, alcohol, and most organic solvents
- Purity
- 99%
- Other Names
- 1-Methylpiperazine, N-Methyl-hexahydropyrazine
- Structural Formula
- CH3N(C4H10N)
- HS Code
- 29333990
- Smell
- Amine-like, characteristic odor
- Poisonous
- Yes
- Molecular Weight
- 100.16 g/mol
- Refractive Rate
- n20/D 1.453
- Ph Level
- Not applicable (basic in solution)
- Shape
- Liquid
- Density
- 0.912 Gram per cubic centimeter(g/cm3)
- Melting Point
- -1C
- Molecular Formula
- C5H12N2
- Form
- Clear, colorless to pale yellow liquid
- Storage
- Store in a tightly closed container, in a cool, dry, well-ventilated area
- Boiling point
- 157-159C
- Classification
- Amine, Heterocyclic compound
- Chemical Name
- N-Methylpiperazine
- CAS No
- 109-01-3
- EINECS No
- 203-624-3
- Grade
- Industrial Grade
- Standard
- Meets industry standards
- Type
- Chemical intermediate
- Usage
- Industrial, laboratory, specialty chemicals
- Main Material
- N-Methylpiperazine
- Application
- Pharmaceutical intermediates, organic synthesis, corrosion inhibitors, agrochemicals
- Non Toxic
- Yes
- Vapor Pressure
- 2.4 mmHg at 25C
- Precautions
- Use with adequate ventilation, avoid contact with skin and eyes
- Stability
- Stable under recommended storage conditions
- Auto-ignition Temperature
- 323C
- Viscosity
- Low viscosity
- Packing
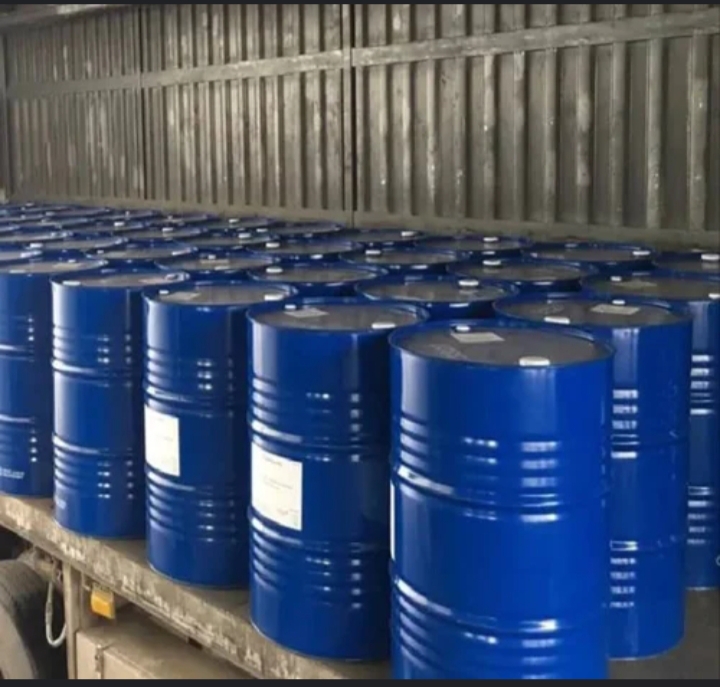
- Available in 200 kg HDPE/steel drums
- UN Number
- 2734
- Shelf Life
- 2 years in unopened packaging
- Hazard Statements
- Irritating to skin, eyes, and respiratory system
- Flash Point
- 45C (closed cup)
N- methylpiperazine About
a heterocyclic organic compound and secondary amine with the chemical formula CHN. It is a critical chemical intermediate heavily utilized in industrial and pharmaceutical synthesis.Versatile Chemical Intermediate
N-Methylpiperazine is widely used across various industries for its efficacy as an intermediate in organic synthesis. Its key roles span pharmaceutical manufacturing, agrochemicals, and corrosion inhibitor production. Its reliability and compatibility with other chemicals make it indispensable for specialty chemical processes requiring high purity and specific chemical properties.
Safe Handling and Storage Guidelines
Due to its potential toxicity and irritant nature, it is important to handle N-Methylpiperazine with care. Use adequate ventilation, avoid direct contact with skin or eyes, and always store the sealed container in a cool, dry, and well-ventilated environment, away from heat and ignition sources. Adhering to these safety practices will maintain the product's quality and ensure the safety of personnel.
FAQ's of N- methylpiperazine:
Q: How should N-Methylpiperazine be safely stored and handled?
A: Store N-Methylpiperazine in tightly closed containers, preferably in a cool, dry, and well-ventilated area. Avoid direct exposure to heat or open flames. When handling, use protective gloves, eye protection, and ensure good ventilation, as it can cause irritation to the skin, eyes, and respiratory system.Q: What are the main industrial uses of N-Methylpiperazine?
A: N-Methylpiperazine serves as an essential intermediate in pharmaceutical production, organic synthesis, agrochemicals, and corrosion inhibitors. Its chemical properties make it crucial for various specialty chemical formulations in laboratory and industrial settings.Q: When does the product reach the end of its shelf life?
A: N-Methylpiperazine retains its quality for up to 2 years when kept unopened in its original packaging and stored under the recommended conditions. Always check the packaging date before use to ensure optimal performance.Q: Where is this product typically used or applied?
A: This chemical is widely used in laboratories, industrial manufacturing plants, and research facilities, particularly in processes involving the synthesis of pharmaceuticals, agrochemical formulations, and the creation of specialty chemicals.Q: What are the key benefits of using N-Methylpiperazine in chemical processes?
A: Its high purity (99%), low viscosity, and complete miscibility with water and most organic solvents enable efficient processing, improved reaction yields, and ease of integration into various chemical syntheses, offering reliability and consistency in industrial and laboratory applications.Q: Is N-Methylpiperazine toxic, and what precautions are necessary during handling?
A: Yes, N-Methylpiperazine can be toxic if ingested or inhaled and is classified as irritating to skin, eyes, and the respiratory system. Always use personal protective equipment and avoid direct contact or breathing vapors during handling.Tell us about your requirement

Price:
Quantity
Select Unit
- 50
- 100
- 200
- 250
- 500
- 1000+
Additional detail
Mobile number
Email

More Products in Industrial Chemical Category
mono ethanol amine
Price 150.0 INR / Kilograms
Minimum Order Quantity : 200 Kilograms
Purity : 99%
Classification : Organic Chemicals
Grade : Industrial Grade
HS Code : 29221110
Technical Grade Urea
Price 80.0 INR / Kilograms
Minimum Order Quantity : 200 Kilograms
Purity : 99%
Classification : Organic Chemicals
Grade : Industrial Grade
HS Code : 31021000
N Methyl Morpholine
Price 250.0 INR / Liter
Minimum Order Quantity : 300 Liters
Purity : 99%
Classification : Organic Chemicals
Grade : Industrial Grade
HS Code : 29349990
Propylene Glycol Usp
Price 100.0 INR / Kilograms
Minimum Order Quantity : 200 Kilograms
Purity : 99%
Classification : Organic Chemicals
Grade : Industrial Grade
HS Code : 29053200

Nirva Speciality Chemicals
All Rights Reserved.(Terms of Use)
Developed and Managed by Infocom Network Private Limited.
Developed and Managed by Infocom Network Private Limited.