Send Inquiry
MIPA 70%
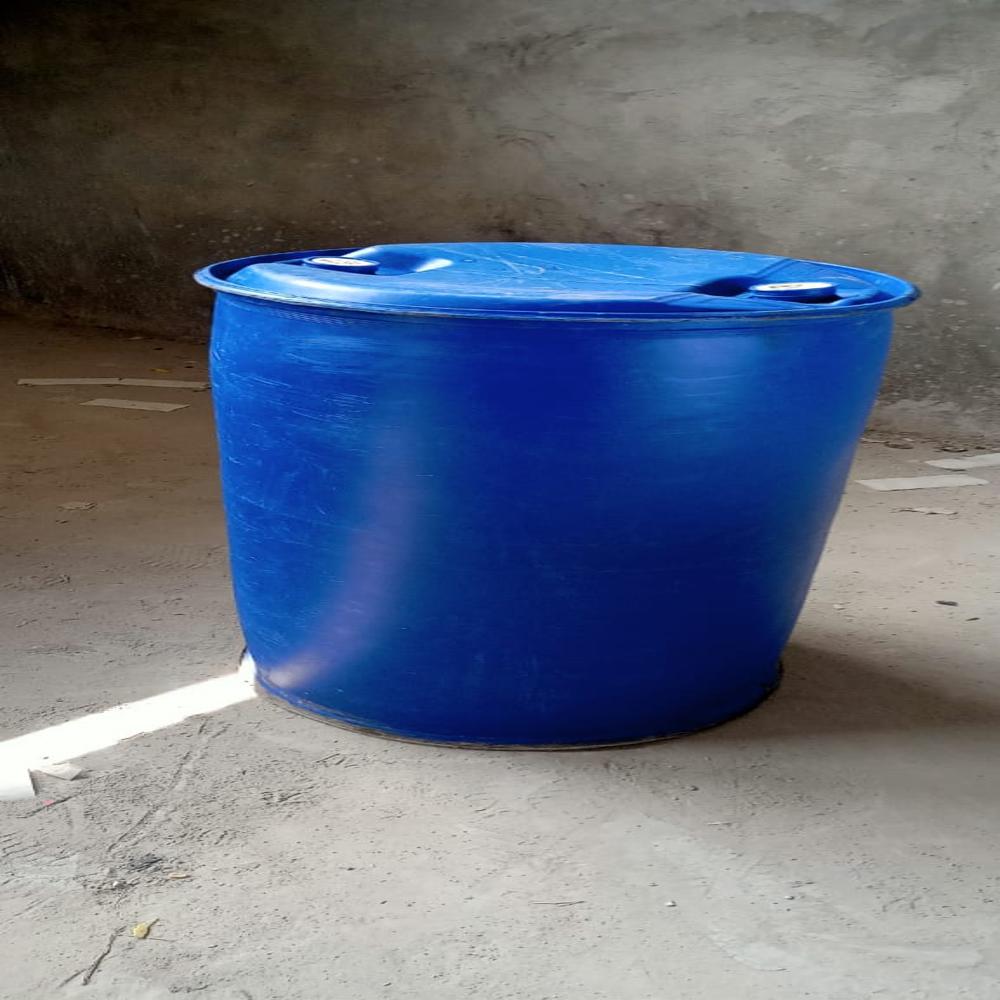

MIPA 70% Specification
- Purity
- 99%
- Chemical Name
- MIPA 70%
- Grade
- Industrial Grade
- Usage
- an industrial-grade aqueous solution containing 70% monoisopropylamine and 30% water. It is a highly versatile chemical intermediate recognized by its mild ammonia-like odor.
- Application
- Industrial
MIPA 70% About
an industrial-grade aqueous solution containing 70% monoisopropylamine and 30% water. It is a highly versatile chemical intermediate recognized by its mild ammonia-like odor.Versatility in Industrial Applications
Thanks to its high purity and reliable composition, MIPA 70% is employed in an extensive range of processes, from agricultural chemical formulation to the production of coatings and pharmaceuticals. Its adaptability makes it essential for industries seeking a consistent, functional intermediate.
Optimal Safety and Handling Protocols
MIPA 70% is formulated to meet industrial standards, emphasizing safe transportation and ease of storage. Experts recommend using appropriate personal protective equipment and adhering to specialized guidelines for handling and disposal to maintain workplace safety.
FAQ's of MIPA 70%:
Q: How is MIPA 70% typically used in industrial applications?
A: MIPA 70% acts as a chemical intermediate and is commonly utilized in the synthesis of agrochemicals, pharmaceuticals, coatings, and other specialty chemicals, offering a stable, aqueous solution for further processing steps.Q: What makes MIPA 70% beneficial compared to other industrial amines?
A: Due to its high 99% purity and controlled 70% concentration, MIPA 70% provides predictable performance, straightforward handling, and enhanced compatibility in a variety of manufacturing environments.Q: When should MIPA 70% be stored or transported with extra caution?
A: MIPA 70% requires careful handling during storage and transport, particularly in well-ventilated, temperature-controlled environments to prevent exposure to heat, direct sunlight, or incompatible substances.Q: Where is MIPA 70% mainly applied?
A: This solution is primarily utilized in chemical plants, manufacturing facilities, and laboratories that produce coatings, agricultural chemicals, pharmaceuticals, and cleaning agents.Q: What is the process for using MIPA 70% in formulations?
A: Manufacturers typically dilute or react MIPA 70% as a raw material in various synthesis processes to develop products tailored to specific industrial needs, while ensuring proper safety protocols are followed.Q: What are the key benefits of utilizing MIPA 70% as a chemical intermediate?
A: It offers high reactivity, excellent solubility in water, and a mild odor, making it safer and more versatile for operators while supporting efficient process integration across multiple sectors.Tell us about your requirement

Price:
Quantity
Select Unit
- 50
- 100
- 200
- 250
- 500
- 1000+
Additional detail
Mobile number
Email

More Products in Industrial Chemical Category
Triethyl benzyl ammonium chloride
Price 300.0 INR / Kilograms
Minimum Order Quantity : 300 Kilograms
Application : Industrial
Melting Point : 185 C
Grade : Industrial Grade
Purity : 99%
GLUCONO DELTA LACTONE
Price 180.0 INR / Kilograms
Minimum Order Quantity : 200 Kilograms
Application : Industrial
Melting Point : 150 C
Grade : Industrial Grade
Purity : 99%

1 4 Dioxane
Price 100.0 INR / Kilograms
Minimum Order Quantity : 300 Kilograms
Application : Industrial
Melting Point : 11.8 C
Grade : Industrial Grade
Purity : 99%
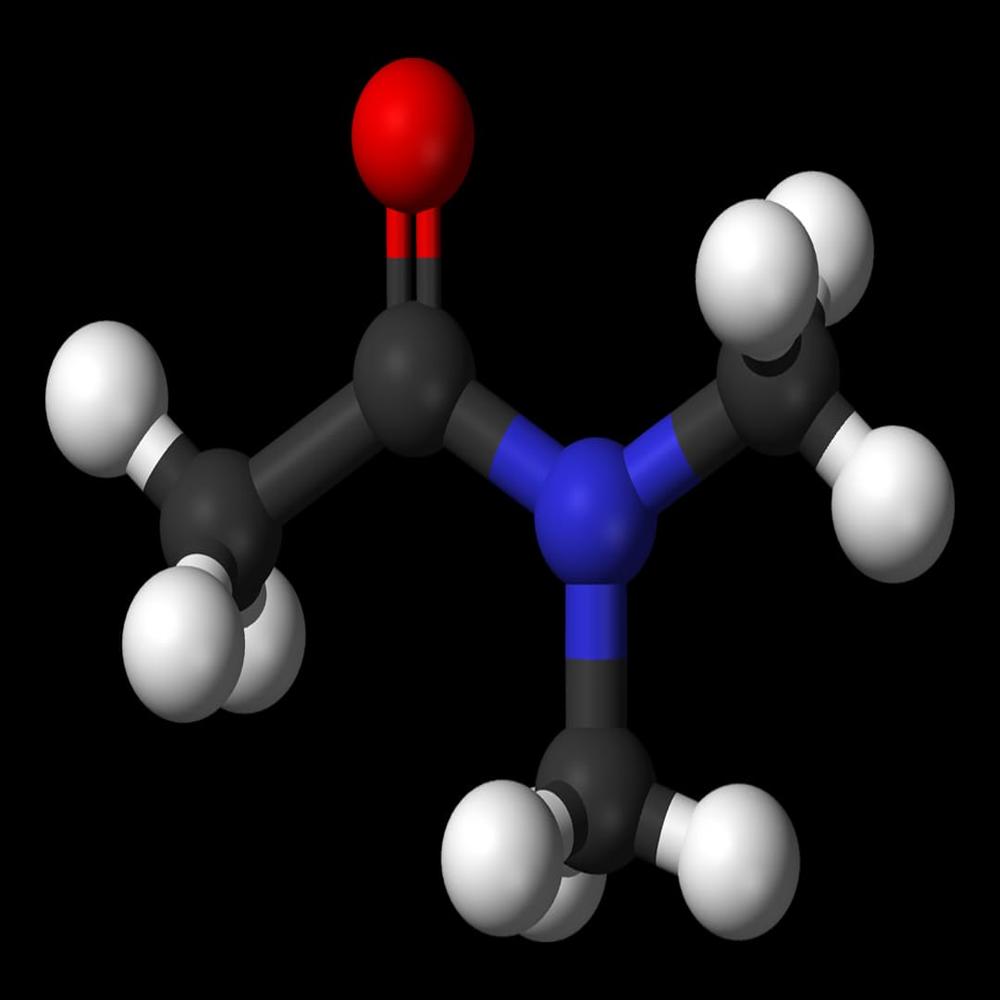
N N Dimethylacetamide
Price 110.0 INR
Minimum Order Quantity : 200
Application : Industrial
Melting Point : 20 C
Grade : Industrial Grade
Purity : 99%

Nirva Speciality Chemicals
All Rights Reserved.(Terms of Use)
Developed and Managed by Infocom Network Private Limited.
Developed and Managed by Infocom Network Private Limited.